- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
What Is the Best Hydrocarbon Cleaning System from China?
Choosing the best Hydrocarbon Cleaning System from China requires more than comparing prices or viewing polished factory photographs. The right system must match the contaminant, component material, cleaning volume, and required surface condition. Dr. Rajiv Kohli, a respected surface-cleaning researcher, emphasizes: “Effective cleaning begins with understanding contamination, surface material, and process conditions.”
That principle guides this introduction. A reliable Chinese system may combine heated cleaning chambers, controlled hydrocarbon solvents, filtration, vacuum drying, and solvent recovery. Picture a metal part leaving the chamber clean, dry, and free from oily residue. The result should be measurable, not merely attractive.
Look for documented cleaning performance, stable temperature control, sealed operation, and clear maintenance procedures. Ask whether the supplier provides test cleaning, process validation, spare parts, operator training, and technical support after installation. These details often reveal more than a low quotation.
Safety also deserves close attention. The equipment should support appropriate ventilation, fire prevention, electrical protection, and local compliance requirements. Certification must be verified for the destination market. Do not rely only on a brochure.
The “best” choice is rarely the cheapest machine. It is the system that delivers repeatable results without creating hidden operating problems. A cheaper offer may conceal higher solvent consumption or difficult maintenance. That risk is easy to underestimate.
This review will compare Chinese manufacturers through practical criteria, including cleaning quality, automation, energy use, safety design, customization, and after-sales reliability. No supplier is perfect. Real factory conditions can expose weaknesses that demonstrations do not show. Careful testing remains essential before making a final decision.
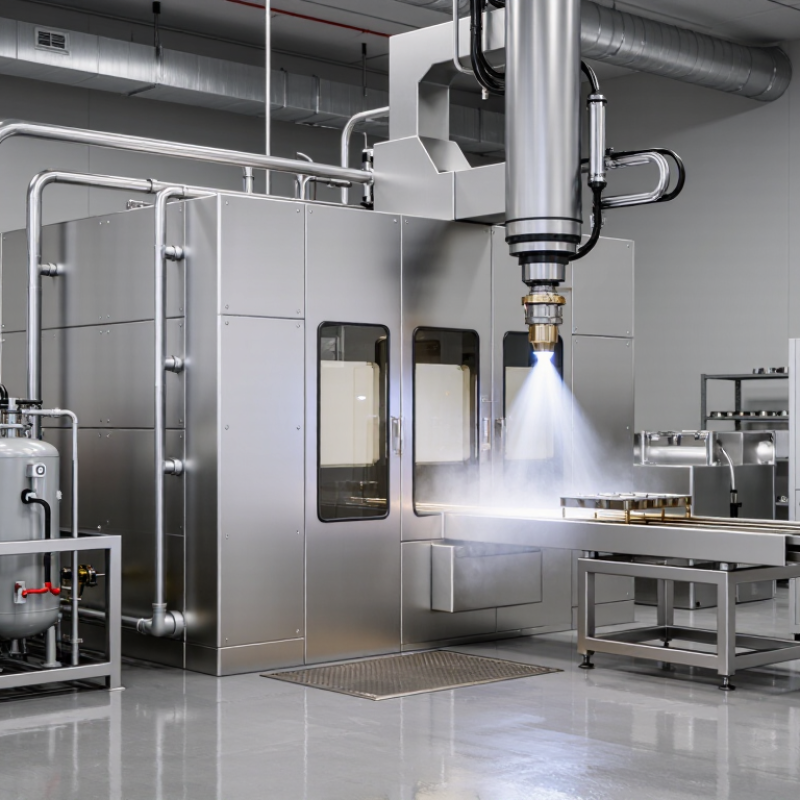
Table of Contents [Hide]
Define Hydrocarbon Cleaning and Its Role in Precision Manufacturing
Hydrocarbon cleaning uses refined, non-water-based solvents to remove oil, grease, wax, and machining residue. These solvents dissolve contamination without swelling many metal components. The process often uses sealed chambers, vacuum drying, filtration, and controlled vapor recovery.
In precision manufacturing, cleanliness affects fit, friction, coating adhesion, and electrical reliability. A bearing race may look bright but still hold a thin oil film. That film can change measured torque or attract abrasive dust.
Technicians therefore check particle levels, surface residues, and drying performance, not appearance alone. Small details matter.
The best hydrocarbon cleaning system from China should match the part, solvent, production volume, and compliance requirements. A reliable system needs stable temperature control, effective filtration, leak protection, and repeatable solvent separation. It should also provide clear operating records and accessible maintenance points.
Poor ventilation or weak sealing can create avoidable risks. In real production, cycle speed is not everything. Excessive speed may leave residue inside blind holes.
My own view is that equipment selection often underestimates loading patterns and part geometry. That weakness deserves a practical trial. Test parts should include difficult surfaces, narrow gaps, and the heaviest expected contamination. Engineers can then compare cleanliness, drying time, solvent consumption, and process stability before approval.