- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
What Is the Best Iron Pipe Bending Machine to Buy?
Choosing the best Iron Pipe Bending Machine starts with your actual workshop demands, not a glossy product photograph. Pipe diameter, wall thickness, material, bend radius, production volume, and available floor space all matter. A compact manual bender may suit occasional repairs. A programmable hydraulic model may be better for repeated structural work.
Metal-fabrication educator Ron Covell offers a useful principle: “Choose the tool that suits the work you actually do.” That advice remains practical. A machine with impressive tonnage can still disappoint when its dies do not match your pipe sizes. The wrong tooling may leave flattened sections, wrinkles, or inconsistent angles. Those defects can appear after several hours of work, when correction becomes expensive.
Look closely at the frame, drive system, die quality, control method, and adjustment range. Feel the machine’s rigidity. Check whether replacement parts are available. Ask how easily operators can repeat a 45-degree or 90-degree bend. Small details matter.
Real production exposes weaknesses.
Your buying decision should also include operator training, maintenance access, warranty support, and electrical requirements. A reliable supplier should provide clear specifications and realistic capacity ratings. Marketing claims need verification through manuals, demonstrations, and customer feedback.
There is no universal winner. The best Iron Pipe Bending Machine is the model that delivers accurate bends, safe operation, and predictable results within your budget. Even experienced buyers can misjudge future workload. Leave room for that uncertainty. A careful comparison now can prevent a costly machine sitting unused beside the workshop wall.
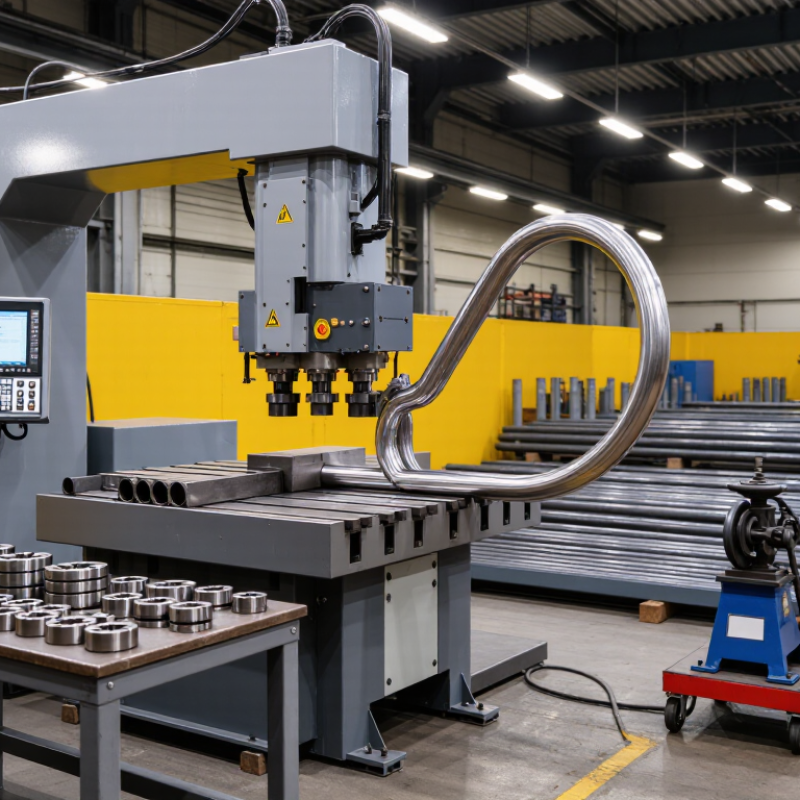
Table of Contents [Hide]
Identify Pipe OD, Wall Thickness, and 1.5D–3D Bend-Radius Requirements
Choosing the best iron pipe bending machine starts with measurements, not machine price. In shop assessments, I record pipe outside diameter (OD), wall thickness, material, and target bend angle. A tube marked “50 mm” may refer to nominal size, not actual OD. That confusion can lead to the wrong tooling. Measure with calipers when possible, then verify the drawing or material record. Small errors become visible at the bend.
Wall thickness affects clamping pressure, mandrel selection, and wrinkling risk. Thin-wall pipe may need a mandrel, wiper die, or pressure die, especially near tight radii. Thick-wall sections demand enough forming force without crushing the pipe. Check the machine’s rated OD and wall-thickness range, not only its maximum diameter. A machine accepting 60 mm pipe may struggle with a 2 mm wall. Test samples matter. They reveal springback, flattening, and surface marks better than a brochure.
Bend radius is usually expressed as a multiple of OD. A 1.5D radius is tight; a 3D radius is gentler and easier to form. Confirm whether the specification means centerline radius, inside radius, or tooling radius. These terms are sometimes used carelessly. I once approved tooling from an unclear drawing, and the finished elbow missed the fit-up dimension. That was avoidable. Request a trial bend using your actual material and wall thickness. Check ovality, angle accuracy, weld-seam behavior, and repeatability across several pieces.