- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
China Top 10 Stainless Steel Stamping Manufacturers?
Choosing a reliable Stainless Steel Stamping manufacturer requires more than comparing factory photos or production claims. This guide examines ten leading Chinese suppliers through practical, measurable criteria. These include material knowledge, tooling capability, dimensional control, surface finish, production capacity, and quality management.
The review considers manufacturers serving industries such as automotive, medical equipment, electronics, construction, and industrial machinery. Attention is given to stainless steel grades, including 304 and 316, because each grade behaves differently during forming. Sheet thickness also matters. A supplier producing small electrical contacts may not suit a deep-drawn enclosure. Details matter.
We also look for evidence of engineering experience, inspection procedures, traceability, and communication quality. Useful signs include coordinate measuring machines, progressive stamping presses, documented first-article inspections, and clear tolerance discussions. Certifications can support credibility, but they should not replace direct technical verification. No list is perfect. Supplier data can change, and published capabilities may not reflect current production conditions.
For buyers, the goal is not simply to find the largest factory. It is to identify a partner that understands tooling wear, springback, burr control, corrosion resistance, and consistent batch production. Requesting samples, drawings, inspection reports, and realistic quotations can reveal important differences. A careful supplier should explain limitations instead of promising everything. That matters.
This overview is designed to support informed comparison. It combines industry-focused research with practical purchasing considerations, while recognizing that final suitability depends on your drawings, volumes, tolerances, and delivery requirements.
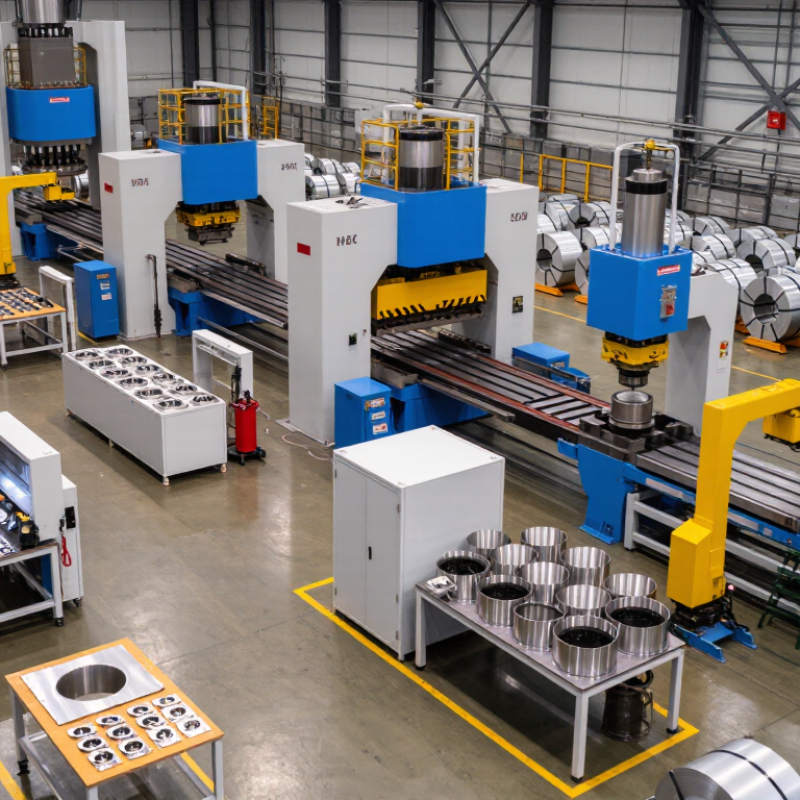
Table of Contents [Hide]
What Is Stainless Steel Stamping?
Stainless steel stamping is a cold-forming process that shapes flat metal sheet with a press and custom-built dies. The machine applies controlled force to cut, bend, draw, or emboss the material. Common parts include brackets, housings, clips, covers, and precision washers. Stainless steel is strong, corrosion resistant, and suitable for demanding environments. However, it is not effortless to form. Its strength can increase during deformation, which may cause cracking or excessive tool wear.
In practical production, engineers check the grade, thickness, grain direction, and required surface finish before designing the die. Grades such as 304 and 316 behave differently during forming. Die clearance must be carefully matched to the sheet. Poor clearance can leave sharp burrs or distorted edges. Progressive dies support high-volume work, while single-operation dies may suit prototypes or smaller batches. Deep drawing requires controlled lubrication and carefully planned forming stages. Otherwise, wrinkles or splits can appear around the walls.
Reliable manufacturers usually verify dimensions with gauges, coordinate measuring equipment, and sample inspections. They also review springback after bending, because the finished angle may shift slightly. A polished drawing does not guarantee a stable production process. Design changes, material variation, and maintenance can still affect results. This is where technical communication matters. Clear tolerances, inspection records, and realistic production trials help reduce avoidable problems when comparing stainless steel stamping manufacturers in China.