- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
China Top Aluminized Steel Coil Manufacturers Suppliers?
Choosing reliable China Top Aluminized Steel Coil Manufacturers Suppliers requires more than comparing online prices. Aluminized Steel Coil combines a steel substrate with an aluminum-based coating, offering heat resistance, surface protection, and practical forming performance. Its quality depends on coating weight, steel grade, thickness tolerance, surface finish, and production control.
This guide examines manufacturers from a buyer’s perspective. It considers factory experience, product range, testing equipment, export records, and communication quality. Experienced suppliers should explain specifications clearly, including coating grades, coil dimensions, mechanical properties, packaging, and delivery terms. Their technical teams should also provide mill certificates, inspection reports, and sample information when requested. Ask for evidence.
A dependable supplier should show how coils are produced and inspected. Useful details include calibrated gauges, laboratory testing, edge condition, weld control, and moisture-resistant packaging. Photos can help, but they are not proof alone. Independent inspection may be appropriate for large orders or demanding applications. Details matter.
No supplier ranking remains perfect for every project. A company suitable for automotive components may not fit furnace parts or roofing applications. Buyers should verify current certifications, production capacity, lead times, and customer references before signing a contract. Some websites also present incomplete or outdated information. That weakness deserves attention. By comparing technical documents, factory evidence, and after-sales responses, purchasers can identify China-based partners with stronger reliability and clearer accountability. The final choice should match the application, budget, compliance needs, and long-term supply expectations.
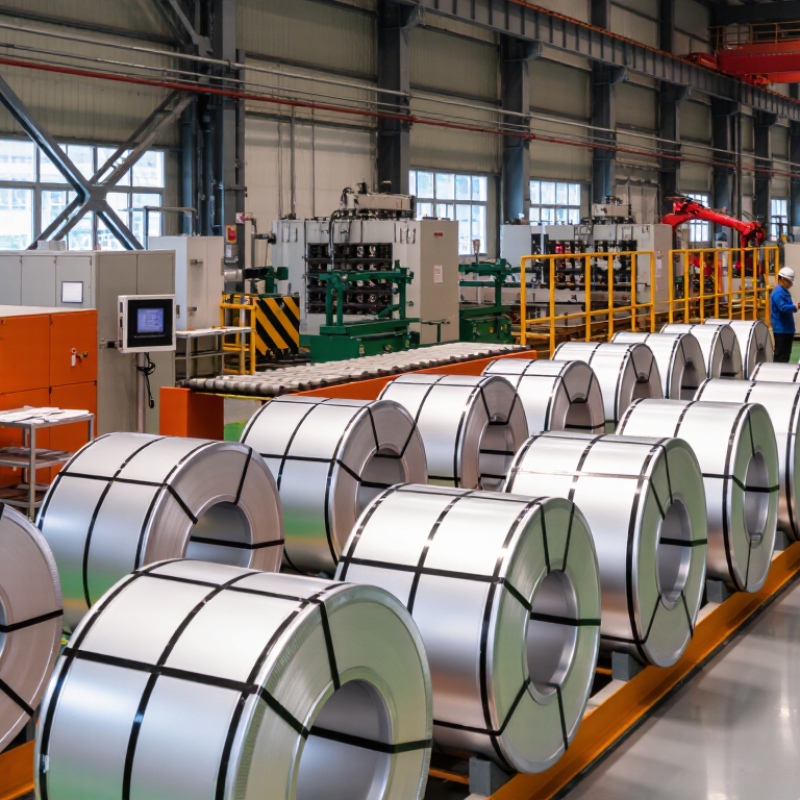
Table of Contents [Hide]
What Defines Aluminized Steel Coil Under ASTM A463 Type 1: 90% Al, 10% Si
ASTM A463 Type 1 defines aluminized steel coil through its coating, not its country of origin. The hot-dip layer contains approximately 90% aluminum and 10% silicon. Aluminum forms a protective oxide film, while silicon helps control iron diffusion during coating. This balance supports heat resistance and atmospheric corrosion protection. It is not stainless steel.
The 2024 USGS Mineral Commodity Summaries estimated global primary aluminum production at about 70 million metric tons in 2023. China accounted for roughly 41 million tons. World Steel Association data recorded approximately 1.89 billion tons of crude steel production worldwide in 2023. These figures show broad raw-material capacity, but they do not prove coil quality. That distinction matters.
When comparing Chinese manufacturers and suppliers, buyers should request ASTM A463/A463M compliance records, coating mass, base-metal grade, coil thickness, width tolerance, and mechanical test results. A coating certificate should identify the Type 1 alloy clearly. Surface appearance also deserves inspection: uneven spangle, edge damage, or exposed steel can signal handling or process problems. Small details matter.
I would not select a supplier from price alone. One overlooked issue is coating adhesion after forming. Ask for bend-test evidence using the intended radius. Some published specifications remain vague. That is a weakness worth challenging before purchase. Reports provide market context; lot-level inspection provides confidence.
China Top Aluminized Steel Coil Manufacturers Suppliers? - What Defines Aluminized Steel Coil Under ASTM A463 Type 1: 90% Al, 10% Si
| Data Dimension | ASTM A463 Type 1 Reference | Practical Coil-Sourcing Information | Quality-Control Point |
|---|---|---|---|
| Product Definition | Hot-dip aluminum-coated steel sheet and coil with a nominal coating composition of approximately 90% aluminum and 10% silicon. | The steel substrate is continuously immersed in a molten aluminum-silicon bath to form a metallurgically bonded coating. | Request the applicable ASTM A463 edition and the material test certificate for each production lot. |
| Coating Type | Type 1 coating: aluminum-silicon alloy coating. | Type 1 is commonly selected for heat resistance, oxidation resistance, reflectivity, and atmospheric corrosion resistance. | Do not substitute Type 2 unless the application specifically requires an aluminum-zinc coating system. |
| Nominal Coating Chemistry | Approximately 90% aluminum and 10% silicon by coating alloy composition. | Silicon helps control the intermetallic layer formed between the coating and the steel substrate during hot-dip processing. | Coating chemistry should be verified through the supplier’s process documentation or inspection certificate. |
| Typical Steel Substrate | Commercial steel, forming steel, drawing steel, and structural grades may be available, depending on the ordered ASTM A463 grade. | Common selection factors include forming severity, required yield strength, tensile strength, elongation, and end-use temperature. | Specify the exact steel grade rather than ordering only “ASTM A463 Type 1.” |
| Coating Designation | ASTM A463 uses “A” coating designations to identify the total coating mass on both sides of the sheet. | Common commercial designations include A40, A60, A80, A100, A130, and A160, subject to availability and product thickness. | Confirm whether the purchase order requires a minimum total coating mass or an average coating mass. |
| Coating-Mass Conversion | An A40 designation corresponds approximately to 0.40 oz/ft² total coating mass, or about 122 g/m² on both sides. | An A60 designation is approximately 183 g/m² total, while A80 is approximately 244 g/m² total. | Coating-mass conversions are rounded; the ASTM designation and test method control acceptance. |
| Available Thickness Range | ASTM A463 covers sheet and coil in a broad range of thicknesses; the permitted range depends on the ordered grade, coating, and production capability. | Industrial supply commonly includes approximately 0.30–3.00 mm, while thinner or thicker material may be available by agreement. | State nominal thickness, permissible tolerance, and whether measurement is taken before or after coating. |
| Available Width Range | Width is normally specified by purchase order and is subject to the producer’s rolling and slitting capability. | Common processing formats include master coils, slit coils, and cut-to-length sheets. | Confirm minimum slit width, inside diameter, outside diameter, coil weight, and width tolerance before ordering. |
| Surface Appearance | The coating should be continuous and reasonably uniform for the ordered coating designation. | Typical surfaces may be supplied as regular mill finish, with controlled surface requirements available for forming or painting applications. | Minor surface variations should be evaluated against the agreed ASTM requirements and approved samples. |
| Heat-Resistance Advantage | The aluminum-rich coating provides strong resistance to oxidation at elevated temperatures compared with ordinary uncoated carbon steel. | Type 1 aluminized steel is widely used in exhaust components, heat shields, furnace parts, ducts, burners, and industrial equipment. | Maximum service temperature depends on stress, atmosphere, forming condition, coating mass, and design; confirm the application temperature separately. |
| Formability | Formability depends primarily on the selected base-steel grade, thickness, coating mass, and bend radius. | Drawing or forming grades are more appropriate for deep-drawn parts than structural grades. | For severe forming, validate bend performance and surface cracking with a production-representative trial. |
| Welding Considerations | Resistance welding, arc welding, and other joining methods can be used with suitable procedures. | Welding may generate fumes and can locally remove or disturb the aluminum-silicon coating. | Use appropriate ventilation, welding parameters, and post-weld corrosion protection where required. |
| Cut-Edge Protection | The aluminum-rich coating can provide sacrificial and barrier protection near exposed edges, but edge performance depends on geometry and environment. | Slit edges, punched holes, and fabricated edges may require additional protection in aggressive environments. | Evaluate cut-edge corrosion for marine, chemical, humid, or high-salt service conditions. |
| Inspection Documents | Material documentation should identify the ASTM A463 designation, steel grade, nominal dimensions, coating designation, and test results. | Useful documents include a mill test certificate, coating-mass test report, dimensional inspection report, and packing list. | Match the certificate heat number, coil number, label, and purchase-order requirements. |
| Recommended Purchase Description | Specify: ASTM A463, Type 1, steel grade, nominal thickness, width, coating designation, surface requirement, coil dimensions, and quantity. | Example: “ASTM A463 Type 1 aluminized steel coil, commercial forming grade, 1.00 mm × 1,250 mm, A60 coating designation, mill finish.” | Include applicable tolerances, packaging requirements, inspection standards, and delivery condition in the purchase order. |
Note: ASTM A463 requirements vary by ordered steel grade, thickness, coating designation, and applicable specification edition. Final purchasing decisions should be based on the current standard, the agreed purchase order, and lot-specific inspection documentation.