- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
Top Carbide Wear Plate Manufacturers and Suppliers
Carbide Wear Plate is a critical material for equipment exposed to severe abrasion, impact, and sliding wear. It commonly protects crushers, chutes, hoppers, excavator buckets, and conveyor transfer points. In these applications, a few millimeters of lost surface can reduce throughput, increase maintenance hours, and contaminate processed material.
The demand context is substantial. World Steel Association reported global crude steel production of approximately 1.89 billion tonnes in 2023, supporting continued activity across mining, fabrication, and heavy industrial supply chains. The U.S. Geological Survey’s Mineral Commodity Summaries 2025 also identifies tungsten as a strategically important mineral, while tungsten carbide remains a widely used hard phase in demanding wear solutions. These reports do not measure plate quality directly. However, they explain why reliable carbide supply and material traceability matter.
This guide examines top Carbide Wear Plate manufacturers and suppliers through practical criteria. These include carbide chemistry, overlay thickness, hardness testing, welding consistency, backing-plate grade, and documented quality controls. Site conditions matter too. A plate facing sharp impact may fail if it is selected only for maximum hardness. That lesson is easy to overlook. Supplier claims should therefore be checked against test certificates, application records, and independent inspection where possible. Product data can also vary between regions and production batches. No ranking is universal. Still, comparing technical evidence, service response, customization capability, and lifecycle value can help buyers choose plates that survive longer beside real transfer chutes, dusty crushers, and vibrating steel structures.
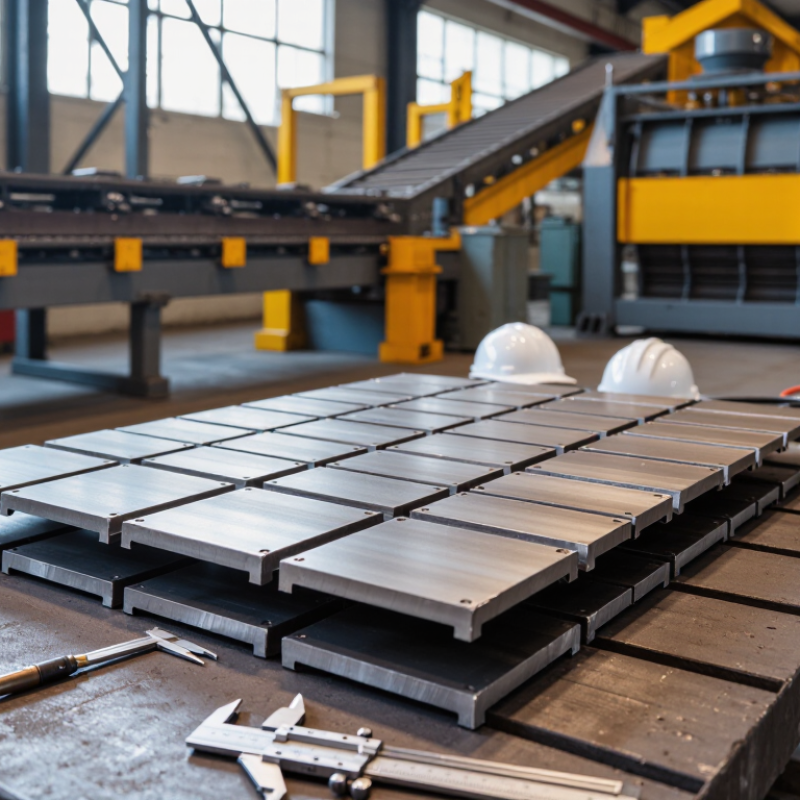
Table of Contents [Hide]
Carbide Wear Plate: Definition, Structure, and Core Properties
Carbide wear plate combines a tough steel backing with hard carbide particles or tiles. The backing absorbs impact, while the carbide phase resists cutting, sliding, and abrasive wear. Common carbide materials include tungsten carbide, bonded with cobalt or nickel-based binders. Particle size matters. Coarse particles usually improve heavy abrasion resistance, while finer particles can support a smoother surface and better edge stability.
The International Tungsten Industry Association reports that cemented carbide consumes roughly 60% of global tungsten use. This figure explains carbide’s importance in mining, recycling, cement, and bulk-material handling.
Plate performance depends on carbide volume, binder content, particle spacing, and bond quality. It is not only about hardness. ASTM G65 testing is widely used to compare dry-sand abrasion loss, but laboratory results cannot fully represent impact, heat, or field contamination.
A hard plate may still crack.
During inspection, exposed carbide islands should appear evenly distributed, without large unbonded gaps or deep transverse cracks. Excessive heat during cutting or welding can weaken the surrounding matrix. This risk is often underestimated.
The USGS Mineral Commodity Summaries identifies tungsten as a strategically important material, with global supply affected by mining concentration and processing limits. That pressure encourages thinner designs, but reduced thickness can lower impact tolerance. Careful selection should match particle size and plate structure to the actual wear mechanism, not merely the highest advertised hardness.