- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
Top 360 Degree Swivel Stand Manufacturers?
Choosing among the top 360 degree swivel stand manufacturers requires more than comparing prices and polished product photos. Buyers must examine rotation smoothness, load capacity, locking strength, base stability, and long-term wear. A stand may turn beautifully on day one, then develop side-to-side movement after months of repeated use. That detail matters.
Mechanical engineer and mounting-systems consultant David P. Smith explains, “A reliable swivel stand should move easily, stop firmly, and remain stable under repeated daily use.” This practical standard helps separate serious manufacturers from short-term suppliers. Strong companies usually provide material specifications, torque data, quality-control procedures, and realistic installation guidance. They also explain whether their 360 degree swivel stand uses steel bearings, polymer bushings, or a sealed rotating plate. These differences affect noise, maintenance, and service life.
This article examines manufacturers through an experience-based lens. It considers factory capabilities, customization options, testing methods, warranty support, and industry reputation. Product consistency deserves attention, especially when stands support monitors, displays, cameras, or retail equipment. A low-cost model can appear attractive. However, unstable movement can create service problems later. That assumption can be wrong when a supplier offers excellent testing and traceable materials. Buyers should still verify every claim. A catalogue is not proof. Sample testing, customer references, and clear technical drawings reveal more. Some manufacturers also overlook cable routing, creating a messy installation around the rotating joint. It is a small flaw, but it affects daily usability. The following overview aims to identify dependable manufacturers while acknowledging that no supplier fits every application.
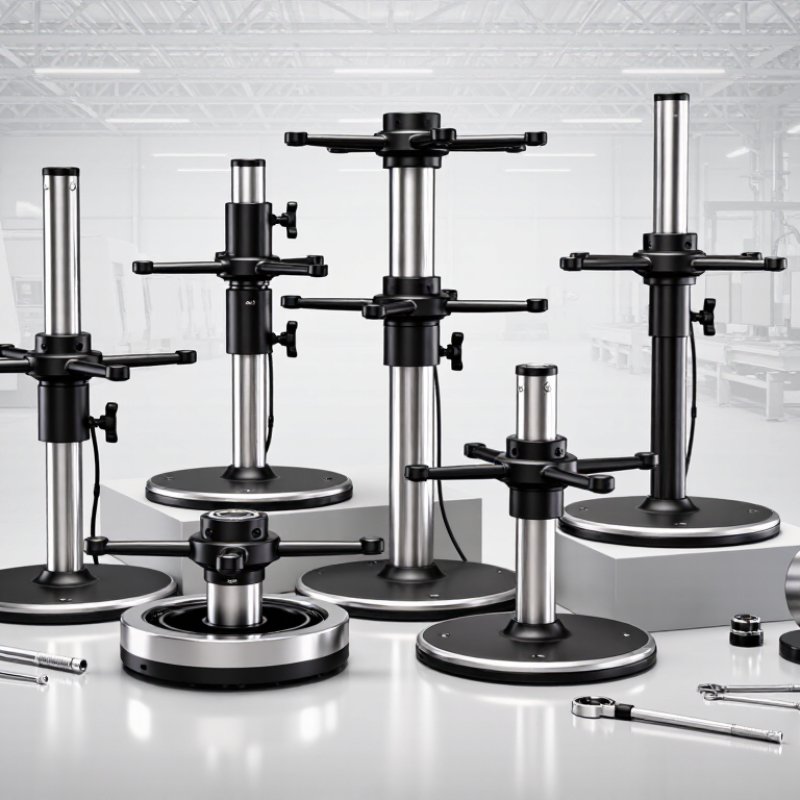
Table of Contents [Hide]
What Is a 360-Degree Swivel Stand and How Does It Work?
A 360-degree swivel stand is a support platform that rotates through a full circle. It can hold a display, monitor, camera, tool, or compact fixture. The stand usually combines a base, rotating plate, central shaft, and bearing assembly. Some models also include a locking knob or indexed positions. These parts keep movement controlled instead of loose or unpredictable.
When force reaches the platform, the bearing transfers the load around the shaft. This reduces friction and allows smooth rotation with modest hand pressure. The base spreads weight across the table or floor. A locking mechanism then fixes the chosen angle. In practical use, I check for wobble by turning the platform slowly and pressing each edge. Uneven resistance often indicates poor alignment, a damaged bearing, or an overloaded stand. Small details matter.
Manufacturers with strong engineering practices publish load ratings, rotation limits, material specifications, and maintenance guidance. Look for steel or reinforced aluminum where stiffness is important. Rubber feet can reduce sliding and vibration on polished surfaces. However, a higher weight rating does not guarantee better operation. The load may sit too high, creating tipping force during rotation. I once underestimated this effect on a tall fixture; the stand turned smoothly but felt unstable. That experience changed my selection process.