- Home
- A-Z Catalogue
- Products
- Valves
- Cetop
- Manual Directional Valves
- Proportional Valves
- Poppet Valves
- High-Speed Linear Servo Valves
- All High-Speed Linear Servo Valves
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10
- Cetop 10 (NG32) Two Stage Type High Speed Linear Servo Valves – LSVHG-10 (With Fail-Safe)
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06
- Cetop 8 (NG25) Two Stage Type High Speed Linear Servo Valves – LSVHG-06 (With Fail-Safe)
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04
- Cetop 7 (NG16) Two Stage Type High Speed Linear Servo Valves – LSVHG-04 (With Fail-Safe)
- Cetop 5 (NG10) Direct Type High Speed Linear Servo Valves – LSVG-03
- Cetop 5 (NG10) OBE Type Direct Operated Linear Servo Valves – LSVG-03-EH
- Cetop 3 (NG6) OBE Type Direct Operated Linear Servo Valves – LSVG-01-EH
- Pumps
- Pressure control
- Flow Control Valves
- Pressure Control Valves
- All Pressure Control Valves
- Brake Valves
- Direct Relief Valve
- Low Noise Solenoid Controlled Relief Valves
- Low Noise Pilot Operated Relief Valves
- Pilot Operated Relief Valves
- Pressure reducing and relieving valves
- Pressure reducing and check valves
- Pressure control valves
- Remote Control Relief Valves
- Solenoid Controlled Relief Valves – BSG
- Solenoid Controlled Relief Valves – BST
- Unloading relief valves
- Check valves
- Environmental
- Valves
- Hydraulic Systems
- Power pack
- About Us
- Contact
- Blog
Top 10 Carbon Steel Shaft Types for Global Buyers?
Choosing the right Carbon Steel Shaft begins with the load, speed, environment, and machining process.
Global steel output provides useful context. The World Steel Association reported approximately 1.88 billion tonnes of crude steel production in 2024. That enormous production base supports diverse shaft grades, from plain carbon steel to alloyed 4140 options. The U.S. Geological Survey’s Mineral Commodity Summaries 2025 also records iron ore production above two billion tonnes worldwide. These figures show the scale behind today’s shaft supply chains. They do not guarantee consistent quality.
Dr. George Krauss, a widely cited steel metallurgist, wrote, “The properties of steel are determined by its microstructure.” That principle matters on the factory floor. A 30-millimeter shaft may look flawless, yet hidden decarburization can reduce fatigue resistance. Poor straightness can also create vibration in a conveyor gearbox. Surface finish matters too. ASTM A108 and ASTM A29 provide useful material and dimensional references, but buyers still need supplier-specific inspection records.
This guide examines ten shaft types used by global buyers. It compares material grades, heat treatment, surface protection, machining needs, and typical applications. Some choices are obvious. Others are not.
A low-cost shaft can become expensive after premature wear, rework, or shipment delays. My experience reviewing industrial components suggests that documentation deserves the same attention as tensile strength. Still, no universal ranking fits every plant. Humidity, shock loading, tolerance requirements, and maintenance skills can change the best choice. Use this list as a practical starting point, not a substitute for engineering validation.
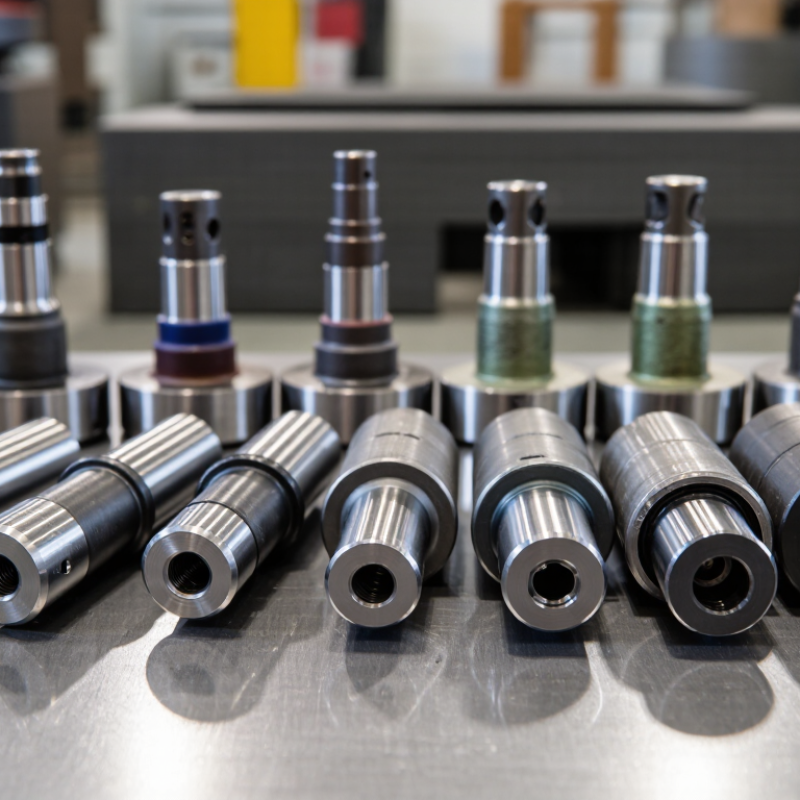
Table of Contents [Hide]
Carbon Steel Shaft Classification: AISI Grades, ASTM Standards, and 570–700 MPa Strength
Top 10 Carbon Steel Shaft Types for Global Buyers
Carbon steel shafts are commonly classified by AISI grades and ASTM requirements. Popular choices include AISI 1018, 1020, 1030, 1040, 1045, 1050, 1060, 1075, 1080, and 1095. Lower-carbon grades offer easier machining and welding. Higher-carbon grades provide greater hardness and wear resistance, but they can be less forgiving during fabrication. AISI 1045 is widely selected for general shafts, pins, rollers, and drive components.
The 570–700 MPa range needs careful interpretation. It may describe tensile strength, yield strength, or a tested condition after heat treatment. These values change with diameter, cooling rate, surface condition, and processing history. ASTM A29 can define general requirements for hot-wrought carbon steel bars, while ASTM A108 commonly covers cold-finished bars. The standard does not replace the material test report. A neat grade chart is not enough.
Tips: Ask suppliers to state the AISI grade, ASTM specification, heat-treatment condition, diameter, and measured mechanical values. Check whether 570–700 MPa means yield or tensile strength. For larger shafts, verify core hardness, straightness, and ultrasonic inspection requirements. In practice, many purchasing errors come from unclear terminology. One detail gets missed. A shaft may meet the grade, yet fail the actual load requirement. Weldability also deserves attention, especially with higher-carbon grades.